When your end mill, drill, or reamer performance depends on the blank it starts from, dimensional precision is not optional — it is the foundation.
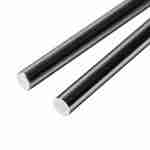
JYC Carbide manufactures solid finished carbide rods ground to H5/H6 tolerance with surface finish Ra ≤ 0.2μm, giving tool grinders and CNC cutting tool manufacturers a reliable, consistent starting point for every production run. With over 30 years of carbide manufacturing experience and a fully integrated production facility, JYC delivers finished rods that meet the exacting standards demanded by European, North American, and Asian tool makers alike.

What Is a Solid Finished Carbide Rod and How It Differs from Blanks
A carbide blank rod is sintered to near-net shape but has not been precision ground. A solid finished carbide rod has been centerless ground to tight dimensional tolerances — typically H5 (±0.003mm) or H6 (±0.005mm) — and is ready for direct use as a cutting tool blank without additional pre-processing.
This distinction matters on the production floor. Finished rods reduce setup time, eliminate pre-grinding steps, and deliver repeatable diameter consistency across batches — critical for high-volume carbide end mill or drill manufacturing. When a batch of 500 end mill blanks all arrive within ±0.003mm of nominal diameter, your collet clamping force, grinding wheel dress cycle, and finished tool runout all become predictable variables rather than sources of scrap.
Beyond diameter, straightness is equally important. JYC finished rods are held to a straightness tolerance of ≤0.03mm per 100mm length, ensuring that the blank does not induce runout before the grinding operation even begins. This is a specification many lower-cost suppliers omit entirely — and tool grinders notice the difference immediately when they load the first piece. For a deeper understanding of how cemented carbide material properties affect tool performance, our technical resource covers the full picture.
Available Specifications – Diameter, Grade, Tolerance and Length
| Parameter | Specification |
|---|---|
| Diameter Range | 1mm – 25mm |
| Grade | K10 / K20 / K30 / Submicron |
| Cobalt Content | 6% – 12% (grade dependent) |
| Tolerance | H5 (±0.003mm) / H6 (±0.005mm) |
| Surface Finish | Ra ≤ 0.2μm |
| Standard Lengths | 100mm / 150mm / 200mm / 330mm |
| Custom Lengths | Available on request |
| Coolant Hole | Available for selected diameters |
All rods are 100% inspected for diameter, straightness and surface finish before shipment. Certificate of conformance available with every order.
Applications – What These Rods Are Used to Produce
Solid finished carbide rods from JYC are used by tool manufacturers worldwide to produce:
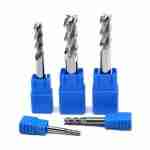
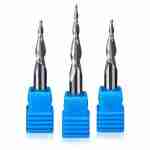
- Solid carbide end mills — 2 flute, 4 flute, ball nose carbide end mill, corner radius, long reach
- Solid carbide twist drills — standard and coolant-through carbide drills
- Carbide reamers — including aerospace-specification finish reamers
- Carbide burrs and rotary files
- Medical and surgical tool blanks — where dimensional consistency is critical for medical device machining
- Customized carbide tools — OEM special-profile designs welcome
The end-use application directly determines which grade and tolerance class you should specify. A 6mm diameter four-flute end mill destined for 45HRC mold steel demands a submicron grade rod with H5 tolerance. A 12mm general-purpose drill for structural steel fabrication may be entirely satisfied by K20 at H6. Understanding this relationship between blank specification and finished tool performance is where JYC’s technical support team adds real value — guiding customers to the most cost-effective specification for each application rather than defaulting to the tightest tolerance for every order.
Diameter Tolerance and Surface Finish Ra Value Explained
The difference between H5 and H6 tolerance affects how the rod seats in your tool grinding collet and ultimately influences runout on the finished tool.
- H6 tolerance (±0.005mm): Suitable for standard end mill and drill production where runout below 0.01mm is acceptable.
- H5 tolerance (±0.003mm): Recommended for micro tools (diameter below 3mm), precision reamers, and aerospace tooling where runout must be held below 0.005mm.
Surface finish Ra ≤ 0.2μm ensures that the rod surface does not introduce stress concentration points that could initiate micro-fractures during grinding or in service. This is particularly relevant for submicron grade rods used in high-speed machining applications — where surface micro-defects on the blank can translate directly into premature edge chipping on the finished tool, even when the grinding operation itself is performed correctly.
It is also worth noting that Ra ≤ 0.2μm has a practical implication for coating adhesion. PVD and CVD coatings applied to finished end mills and drills adhere more uniformly to tools ground from smooth-surface blanks. Tool makers who coat their products in-house consistently report improved coating adhesion and more uniform layer thickness when switching from unground blanks to JYC precision-finished rods. To understand how blank quality ties into overall tungsten carbide tool life, our detailed guide walks through every contributing factor.
Grade Selection Guide – K10 vs K20 vs K30 vs Submicron
| Grade | Cobalt % | Hardness (HRA) | Best For |
|---|---|---|---|
| K10 | ~6% | ≥91.5 | Finish end mills, reamers, micro drills requiring maximum hardness |
| K20 | ~8% | ≥90.5 | General end mills and drills balancing hardness and toughness |
| K30 | ~10–12% | ≥89.5 | Roughing end mills, heavy-duty drills requiring impact resistance |
| Submicron | ~10% | ≥92.0 | HRC65+ hardened steel tooling, aerospace precision tools |
Grain size is the variable that separates a standard K10 from a submicron grade. JYC ultrafine carbide rods are produced from tungsten carbide powder with a mean grain size of 0.4–0.6μm, compared to 1.0–1.5μm for standard K grades. The finer grain structure delivers higher transverse rupture strength (TRS) alongside elevated hardness — a combination that standard grades cannot match, and which makes submicron the preferred choice for micro-diameter end mills below 2mm and for tooling that machines hardened steel above HRC62.
Not sure which grade fits your application? Send us your tool specification and our technical team will recommend the right grade within 24 hours.
Standard Lengths and Custom Cutting Service
JYC solid finished carbide rods are stocked in four standard lengths to cover the most common tool grinding requirements:
- 100mm — suitable for short end mills and micro drills diameter 1mm–6mm
- 150mm — general purpose end mills and standard drills diameter 4mm–12mm
- 200mm — long reach end mills and deep hole drills diameter 6mm–16mm
- 330mm — ultra-long tooling and multiple-cut blank production diameter 8mm–25mm
Custom lengths are available with minimum order quantities as low as 50 pieces per specification. Lead time for custom lengths is 7–14 business days from order confirmation. For customers who produce multiple tool sizes from a single rod length, JYC also offers a precision cutting service — rods can be supplied pre-cut to your exact blank lengths with square, burr-free ends ready for immediate collet loading. This service eliminates the need for an in-house cut-off station and reduces material waste from saw kerf losses on expensive carbide stock.
OEM Bulk Orders Welcome – Low MOQ 50pcs Available
JYC Carbide works directly with cutting tool manufacturers, tool grinders, and industrial distributors globally. Our OEM carbide tools service covers:
- Custom diameter from 1mm to 25mm in 0.1mm increments
- Custom grade — standard K series or proprietary submicron formulations
- Custom tolerance — H5, H6, or tighter on request
- Custom length — any length from 50mm to 400mm
- Coolant hole options — single or twin hole, custom helix angle
- Private labeling and export packaging available
Minimum order quantity starts at 50 pieces per specification for finished rods. Volume pricing available for orders above 500 pieces. For distributors placing consolidated orders across multiple specifications, JYC offers blanket order agreements with scheduled monthly releases — allowing you to lock in pricing while maintaining flexible call-off quantities aligned to your actual consumption. Learn more about JYC carbide manufacturer advantages and why tool makers across Europe and North America trust JYC as their primary carbide blank supplier.
Request Sample or Submit RFQ
Before committing to a bulk order, JYC offers free sample rods for dimensional verification and grinding trials. To request samples or submit an RFQ, please provide:
- Diameter required (mm)
- Grade preference (K10 / K20 / K30 / Submicron)
- Tolerance required (H5 or H6)
- Length required (standard or custom)
- Coolant hole required (yes/no)
- Estimated monthly volume
Our sales team responds to all RFQ submissions within 24 hours on business days.
Frequently Asked Questions
Q: Solid carbide rod with coolant hole for drill manufacturing — — can I order custom specs?
A:Yes. Single hole, twin hole, and helical coolant holes available. Specify hole diameter, count, and helix angle in RFQ. MOQ 50 pcs. Lead time 7–14 business days.
Q: Carbide rod blanks for end mill grinding — what diameter range is available?
A:1mm to 25mm, in 0.1mm increments. K10, K20, K30, and sub-micron grades stocked. Standard lengths: 100 / 150 / 200 / 330mm. Custom lengths from 50mm to 400mm on request.
Q: What cobalt content is right for carbide rods used to make roughing end mills?
A:10–12% cobalt (K30 grade). Higher cobalt increases toughness and impact resistance — essential for roughing cuts and interrupted cuts. Lower cobalt grades are harder but more brittle under heavy load.


Request a Quote for Carbide Tools