Incoming quality control for indexable carbide cutting tools often comes down to one critical verification: confirming that the physical insert delivered in the box matches the exact ISO designation printed on the packaging label and technical drawing. When mislabeled packages, mixed production lots, or incorrect corner radii bypass receiving inspection, the immediate result is tool holder mismatch, improper tool seating, dimensional scrap on the machining floor, or sudden edge failure during production runs.
ISO 1832 establishes a standardized designation system to simplify purchasing, ordering specifications, and dimensional referencing for indexable inserts. However, reading a code on a purchase order is only the first step. For a quality inspector or procurement quality engineer, the physical part must be validated across its core dimensional positions—specifically inscribed circle (IC), thickness (S), and corner radius (RE)—against the manufacturer’s drawing and ISO code before approving inventory for production.
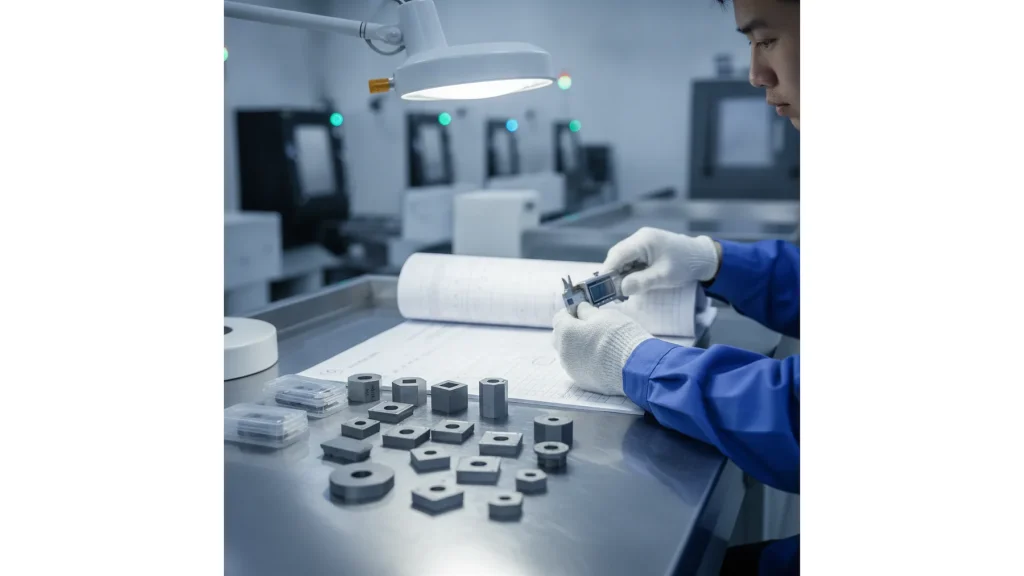
The Receiving Verification Objective: Linking Physical Geometry to the ISO Code
To verify that a carbide insert matches its ISO code, quality personnel must cross-reference the physical insert’s shape, clearance angle, tolerance class, clamping geometry, size (inscribed circle), thickness, and corner radius against the standardized positions defined under ISO 1832.
Accepting an unverified lot risks putting an incorrect corner radius or wrong thickness into an automated machining center, causing immediate tool offset errors or component collisions.
ISO 1832 provides the international baseline for indexable insert designation, standardizing the order and significance of geometry, size, and tolerance symbols.
Inspect a representative sample from every incoming lot by measuring critical reference dimensions and comparing them against the vendor’s drawing and packaging code before signing off on receiving.
In industrial procurement, a carbide insert code functions as a structured dimensional summary. Each position in the standard ISO designation (such as the 7 core positions for standard turning or milling inserts) corresponds to a specific physical feature: insert shape, major clearance angle, dimensional tolerance class, clamping or chipbreaker feature, size (inscribed circle / cutting edge length), thickness, and corner radius.
The primary goal during incoming receiving is not to re-engineer the insert from scratch, but to confirm that the delivered insert’s physical features match the ordered specification. If any physical attribute deviates from the coded symbol, the batch represents either a mislabeled package, a mixed lot, or an out-of-spec production run that warrants immediate quarantine.
Decision checkpoint
- Confirm the packaging label matches the purchase order and technical drawing designation exactly.
- Quarantine the lot immediately if the visual geometry (shape, hole, or major clearance) conflicts with the designation code.
Where Is Insert Tolerance Shown in the Code and How Is It Interpreted?
In standard ISO 1832 designations, insert dimensional tolerance is defined by the third letter position of the code (for example, the ‘M’ in CNMG, ‘G’ in WNGA, or ‘E’ in CCET), which establishes the allowable limits on the inscribed circle, thickness, and profile height.
Assuming that all carbide inserts share the same manufacturing tolerance causes inspection disputes; a ground utility class insert exhibits different allowable deviation than a precision ground finishing insert.
The third letter position of the ISO 1832 system defines specific class boundaries for inner circle (IC), thickness (S), and nose height (M) variation.
Identify the third letter of the incoming designation to determine whether the batch represents a precision-ground tolerance class or a standard molded utility class before evaluating dimensional variance.
The third character in the ISO designation specifies the tolerance class. Tolerance classes dictate allowable deviations for key reference dimensions: the inscribed circle (IC), the insert thickness (S), and the reference dimension from the corner to the theoretical gauge point. Classes with tighter tolerances, such as ground inserts used for high-precision finishing, operate within narrower bands than standard molded utility classes.
When performing incoming verification, inspectors must verify what tolerance class is dictated by the part number. If a drawing requires a precision class insert but the physical package designates a molded class, or if measurements show deviations outside the referenced class specification from the official standard or drawing, the inspector must flag the discrepancy prior to toolholder mounting.
Decision checkpoint
- Check the third letter of the insert code against the purchase specification to confirm whether a ground or utility tolerance class is required.
- Verify that measured thickness and inscribed circle deviations stay within the tolerance class limits designated on the approved drawing.
How to Check Physical Insert Dimensions Against an ISO Code and Drawing
Inspectors check insert dimensions against an ISO code by measuring three critical size-determining features: the inscribed circle (IC) corresponding to the size code position, the insert thickness (S) corresponding to the thickness position, and the corner nose radius (RE) corresponding to the corner radius position.
Mismatched corner radii (such as confusing an 08 / 0.8 mm radius with an 04 / 0.4 mm radius) directly causes surface finish defects, dimensional undersizing, or premature edge chipping on the production line.
Positions 5, 6, and 7 of the standard ISO designation designate the size/edge length, thickness, and corner radius respectively, which can be verified using calibrated metrology tools.
Measure the IC, thickness, and corner radius using appropriate metrology equipment, documenting each value against the drawing nominals and ISO code values.
Verifying physical dimensions against the ISO code requires focusing on the core numeric positions that govern physical fit and cutting geometry:
1. Inscribed Circle (IC) and Edge Length (Position 5): For regular polygonal shapes (such as rhombic, triangular, square, or trigon inserts), the inscribed circle represents the diameter of the largest circle tangent to the insert edges. Calibrated micrometers or precision calipers measure across opposing cutting edges (or specific datum fixtures depending on insert polygon shape). Compare the measured IC against the standardized metric size code (e.g., 12 for a 12.7 mm IC in standard turning inserts).
2. Thickness (Position 6): Insert thickness is measured across the top and bottom locating surfaces using a flat-anvil micrometer or height gauge. The measured thickness must match the numeric thickness code (e.g., 04 representing standard nominal thickness) within the specified drawing and tolerance class limits.
3. Corner Radius (Position 7): The nose radius directly governs tool strength, feed capabilities, and final part finish. Because a visual check cannot reliably distinguish between adjacent radii (such as 0.4 mm, 0.8 mm, or 1.2 mm), inspectors should verify corner radius using an optical comparator, digital toolmaker’s microscope, contour tracer, or precision radius gauges against the vendor drawing profile.
Decision checkpoint
- Use optical or tactile profiling to confirm corner radius; do not rely on naked-eye estimation.
- Verify that the measured thickness matches the nominal pocket depth required by the intended tool holder.
Identifying Mixed Batches, Labeling Errors, and Supplier Deviations
Mixed batches and mislabeled packages are identified by checking physical labeling consistency across inner and outer packaging, verifying edge preparation markings, and conducting random multi-point sampling across each received box.
Discovering a mislabeled batch after tools are distributed to the machine shop floor leads to untracked setup scrap, tool breakage, and complex lot recalls.
Incoming inspection sampling plans isolate packaging discrepancies from actual dimensional manufacturing defects.
Cross-check the outer box label, inner pack label, insert laser markings (if present), and measured physical samples before releasing the lot.
Packaging and handling errors in the supply chain occasionally result in inserts being placed in incorrect plastic boxes or marked with erroneous codes. Common discrepancies detected during incoming quality audits include:
– Mislabeled Corner Radius: The package indicates an 08 radius, but optical inspection reveals an 04 radius inserted into the cavity.
– Incorrect Chipbreaker or Edge Preparation: The ISO code indicates a specific manufacturer chipbreaker or edge preparation (honing, chamfering, or round-edge), but the physical part displays an unhoned sharp edge or different geometry.
– Substrate or Coating Variation: Visual inspection or supplier test reports reveal an uncoated or physical-vapor-deposition (PVD) coated insert where a chemical-vapor-deposition (CVD) multi-layer grade was specified.
When an inspector detects even one non-matching insert within a sampled box, the entire lot must be isolated from production inventory to prevent cross-contamination in shop tooling cribs.
Decision checkpoint
- Cross-reference outer packaging labels, inner pack markings, and physical edge preparation before distributing inserts to production.
- Quarantine the complete package immediately if sample measurements reveal a corner radius or substrate coating mismatch.
Discrepancy Handling and Acceptance/Rejection Workflow
When measured dimensions, tolerance classes, or corner radii do not align with the ISO code or purchasing drawing, the lot must be quarantined, a non-conformance report issued, and formal disposition requested from supplier quality engineering.
Accepting non-conforming inserts under informal deviation agreements without engineering sign-off exposes subsequent CNC operations to unpredictable tool life and dimensional part failures.
Vendor qualification and incoming quality agreements establish baseline acceptance criteria based on standard drawing conformity.
Follow a structured non-conformance workflow: quarantine the physical batch, log the dimensional variance on an incoming inspection sheet, and require vendor verification or replacement.
A structured discrepancy protocol ensures procurement and engineering maintain traceability when received carbide inserts fail dimensional verification:
1. Physical Quarantine: Segregate the entire shipment in a designated non-conforming holding area to prevent accidental release to production tool cribs.
2. Evidence Documentation: Record measured physical dimensions (IC, thickness, nose radius) alongside the packaging designation, batch number, and vendor drawing nominals.
3. Root-Cause Inquiry: Determine whether the issue is a labeling error (correct part in the wrong box), a production dimensional failure (part out of tolerance), or an ordering discrepancy (incorrect code generated during purchase order entry).
4. Supplier Disposition: Present the inspection record to the supplier for formal corrective action, return authorization, or replacement batch delivery.
Decision checkpoint
- Do not modify out-of-spec indexable inserts on shop-floor grinders unless authorized by an approved engineering deviation.
- Request full vendor dimensional inspection reports for recurring batch discrepancies.
Incoming Carbide Insert Dimensional QC Checklist
An effective incoming carbide insert QC checklist verifies the relationship between the physical workpiece, the packaging ISO code, and the drawing specifications across every key geometric position.
Standardizing the inspection checklist ensures consistent acceptance criteria across all receiving shifts and prevents subjective inspection decisions.
Structured inspection tables align physical metrology checks directly with ISO 1832 positional nomenclature.
Implement the standardized inspection checklist below for all incoming indexable carbide cutting tool deliveries.
Quality inspectors should complete this verification checklist for every sample lot before releasing indexable carbide inserts to production.
| Inspection Parameter | ISO Code Position | Verification Method / Tool | Drawing / Code Match Criteria | Result (Pass / Fail) |
|---|---|---|---|---|
| Insert Shape & Major Angle | Position 1 & 2 (e.g., C, D, S, T, W / N, C, P) | Visual inspection / Protractor / Template | Matches standard polygon geometry and specified clearance angle | Verify |
| Tolerance Class Letter | Position 3 (e.g., M, G, E, U) | Dimensional inspection record comparison | Tolerance range adheres to drawing limits and ISO tolerance class | Verify |
| Clamping / Hole Geometry | Position 4 (e.g., G, M, W, T) | Visual inspection / Pin gauge / Caliper | Hole profile, countersink, and chipbreaker placement match code | Verify |
| Inscribed Circle (IC) / Size | Position 5 (e.g., 06, 09, 12, 16) | Calibrated micrometer / Vernier caliper / Optical gauge | Measured IC matches nominal code dimension within drawing tolerance | Verify |
| Thickness (S) | Position 6 (e.g., 02, 03, 04, 06) | Flat anvil micrometer / Height gauge | Measured thickness matches designated thickness within tolerance limits | Verify |
| Corner / Nose Radius (RE) | Position 7 (e.g., 02, 04, 08, 12) | Optical comparator / Toolmaker microscope / Radius gauge | Profile curve matches designated nose radius nominal value | Verify |
| Packaging & Lot Consistency | Label & Box Marking | Cross-verification of outer box, sleeve, and PO | Code strings, batch numbers, and grade markings identical across all units | Verify |
Decision checkpoint
- Ensure every row in the checklist is logged with actual measured numerical values, not just binary checkmarks.
- Archive completed inspection sheets with the lot number for machining traceability.
Frequently Asked Questions
How to verify a carbide insert matches its ISO code?
To verify an insert matches its ISO code, cross-check the outer label against the purchase order, visually confirm the shape and clearance angle, and measure the inscribed circle (IC), thickness, and corner radius using calibrated metrology tools. Compare these physical measurements to the nominal values defined by the corresponding positions in the ISO 1832 designation and vendor drawing.
Where is insert tolerance shown in the code?
Insert tolerance is designated by the third letter in the standard ISO 1832 code (such as the ‘M’ in WNMG or ‘G’ in CCGT). This position defines the permissible dimensional variations for the inscribed circle, thickness, and profile height of the insert.
What should be included in an insert QC checklist?
An insert QC checklist should include basic lot identification (PO number, batch, brand/grade), visual verification of insert shape, clearance, and clamping hole, precise measurements of the inscribed circle (IC), thickness, and corner radius, verification of edge preparation/chipbreaker, and a clear pass/fail disposition record.
How to check insert dimensions against a drawing?
Check insert dimensions against a drawing by mounting the insert on a calibrated optical comparator, toolmaker’s microscope, or tactile measurement fixture. Align the insert against the specified drawing datums, measure the inscribed circle, overall thickness, and corner radius, and verify that the measured values fall within the drawing’s specified upper and lower tolerance limits.
Discuss Your Tooling Requirement
Send the workpiece material, hardness, operation, tool diameter, reach, machine and holder details for a bounded tooling review.
Send your machining requirements to TUNGVARA.