4 Flute End Mill – JYC Carbide

- Shank Dia (mm):4mm 6mm 8mm 10mm 12mm 14mm 16mm 18mm 20mm
- Flute Dia.(mm):1mm – 20mm
- Cutting Length (mm):1mm – 20mm
- Overall Length (mm):50mm – 100mm
- Flutes:1 / 2 / 3 / 4 Flutes
- HRC:HRC 45 / 55 / 60 / 65
- MOQ:1 pcs (standard) / 1-50 pc (custom)
- Quality Standards: DIN 6537 and DIN 6535-HA
Product Details
| Brand | JYC Carbide |
| Model NO. | 4 Flute End Mill |
| Product Item No. | NCG-4E-DE1-20 |
| Material | Tungsten Carbide (WC-Co) |
| Material Cobalt Content | Available for 6%-12% Usually 10%,12% |
| Material Hardness HV30 | Available 1660-2000 Usually 1660, 1700, 1780 |
| Grade | YG6 / YG8 / YL10.2/YK20UF/YK25UF/YK30SF |
| Coating | Uncoated / TiAlN / AlTiN / DLC |
| Grain Size | 0.2-1.0um Usually 0.4um, 0.5um ,0.7um |
| Density | 14.2-14.90 g/cm3, usually 14.2g/cm3, 14.5g/cm3 |
| Tooth Form | Spiral Tooth |
| Tooth Space | Sparse Tooth |
| Inspection Type for Finished Products: | 100% inspection (Visual inspection & Function inspection) |
| Traceability of Raw Materials: | Yes |
| Tolerance | h6 |
| Customization: | Available |
| Laser Logo | Available |
| MOQ | 1 pcs (standard) / 1-50 pc (custom) |
| Lead Time | 3–5 days (standard) / 7–30 days (custom) |
| Certification | ISO 9001 / ISO 14001 / ISO 45001 / ISO 50001 / COC |
| Custom Service | OEM / ODM accepted |
Description
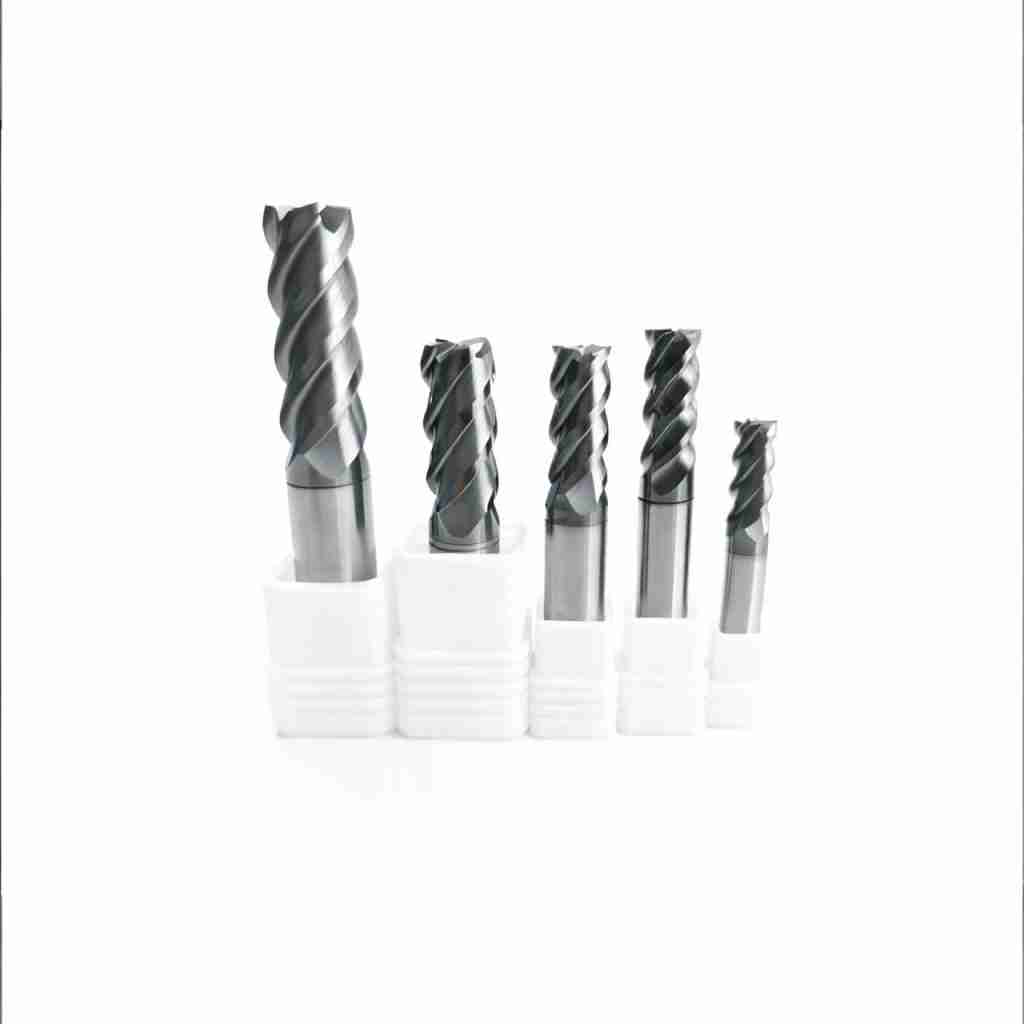
This 4 flute end mill is a general‑purpose solid carbide tool designed for side milling, step milling, and square shoulder machining on steels and other common engineering materials. The 4 flute layout provides more cutting edges in contact with the workpiece than a 2‑flute tool, which helps achieve smoother surface finishes and allows higher feed rates at the same chip load per tooth.
To support precision machining, the cutting diameter is manufactured to tight tolerances: 0 / −0.02 mm for diameters below 12 mm and 0 / −0.03 mm for diameters 12 mm and above. This helps you hold accurate wall locations, step heights, and square corners in demanding applications such as mold bases, fixtures, and precision components. Combined with rigid carbide material and optimized flute geometry, this 4 flute end mill is well suited to a wide range of CNC operations from semi‑finishing to finishing, and fits naturally into broader carbide end mills solutions in your tool crib.
Key Features
- 4 flute geometry provides high rigidity and stable cutting for side milling, step milling, and square shoulder machining on steel and general engineering materials.
- Tight diameter tolerance supports precision fits and accurate shoulders:
- D ≤ 12 mm: 0 / −0.02 mm
- D≥12 mm: 0 / −0.03 mm
- Solid carbide construction offers excellent wear resistance and edge strength, suitable for long production runs in CNC machining centers.
- Short, rigid cutting length helps reduce tool deflection and chatter, improving surface finish and dimensional control on critical features.
- Center‑cutting design allows ramping and light plunging operations when needed, simplifying tool paths in pockets and cavities.
Available Size
| NO. | Order Product No. | Size (mm) | Flutes Z | |||
|---|---|---|---|---|---|---|
| D | Handle D. | Cutting Length | Total Length | |||
| 1 | NCG-4E-D1.0S | 1 | 4 | 3 | 50 | 4 |
| 2 | NCG-4E-D1.5S | 1.5 | 4 | 4 | 50 | 4 |
| 3 | NCG-4E-D2.0S | 2 | 4 | 6 | 50 | 4 |
| 4 | NCG-4E-D2.5S | 2.5 | 4 | 8 | 50 | 4 |
| 5 | NCG-4E-D3.0S | 3 | 4 | 8 | 50 | 4 |
| 6 | NCG-4E-D4.0S | 4 | 4 | 11 | 50 | 4 |
| 7 | NCG-4E-D1.0 | 1 | 6 | 3 | 50 | 4 |
| 8 | NCG-4E-D1.5 | 1.5 | 6 | 4 | 50 | 4 |
| 9 | NCG-4E-D2.0 | 2 | 6 | 6 | 50 | 4 |
| 10 | NCG-4E-D2.5 | 2.5 | 6 | 8 | 50 | 4 |
| 11 | NCG-4E-D3.0 | 3 | 6 | 8 | 50 | 4 |
| 12 | NCG-4E-D3.5 | 3.5 | 6 | 10 | 50 | 4 |
| 13 | NCG-4E-D4.0 | 4 | 6 | 11 | 50 | 4 |
| 14 | NCG-4E-D4.5 | 4.5 | 6 | 11 | 50 | 4 |
| 15 | NCG-4E-D5.0 | 5 | 6 | 13 | 50 | 4 |
| 16 | NCG-4E-D5.5 | 5.5 | 6 | 16 | 50 | 4 |
| 17 | NCG-4E-D6.0 | 6 | 6 | 16 | 50 | 4 |
| 18 | NCG-4E-D7.0 | 7 | 8 | 20 | 60 | 4 |
| 19 | NCG-4E-D8.0 | 8 | 8 | 20 | 60 | 4 |
| 20 | NCG-4E-D9.0 | 9 | 10 | 22 | 75 | 4 |
| 21 | NCG-4E-D10.0 | 10 | 10 | 25 | 75 | 4 |
| 22 | NCG-4E-D11.0 | 11 | 12 | 26 | 75 | 4 |
| 23 | NCG-4E-D12.0 | 12 | 12 | 30 | 75 | 4 |
| 24 | NCG-4E-D14.0 | 14 | 14 | 32 | 75 | 4 |
| 25 | NCG-4E-D16.0 | 16 | 16 | 45 | 100 | 4 |
| 26 | NCG-4E-D18.0 | 18 | 18 | 45 | 100 | 4 |
| 27 | NCG-4E-D20.0 | 20 | 20 | 45 | 100 | 4 |
Non-standard sizes available upon request. Contact us for custom specifications,We will feedback to you within 24 Hours.
Applicability for Materials
◎ = Perfect for ○ = Suit — = N/A
| Carbon Steel | Alloy Steel | Pre-hardened Steel / Hardened Steel | Stainless Steel | Cast Iron / Nodular Cast Iron | Copper Alloy | Aluminium Alloy | Titanium Alloy | Heat-resistant Alloy | |||
|---|---|---|---|---|---|---|---|---|---|---|---|
| ~45HRC | ~50HRC | ~55HRC | ~68HRC | ||||||||
| ◎ | ◎ | ◎ | ○ | — | — | ○ | ◎ | — | — | — | — |
Packaging & Delivery
| Packaging | Individual plastic tube + foam box |
| Port | Shenzhen / Guangzhou /Shanghai |
| Lead Time | 3–5 days (in-stock) / 7–30 days (custom) |
| Shipping | DHL / FedEx / UPS / Sea freight |




Applications / Suitable Uses
- Side milling and profiling of slots, pockets, and external contours where good surface finish and dimensional accuracy are required.
- Step milling to create precise steps and levels on mold plates, machine components, and jigs.
- Square shoulder machining for accurate 90° corners and shoulders in steel parts and general machined assemblies.
- Finishing and semi‑finishing passes on carbon steel, alloy steel, stainless steel, and cast iron after roughing with lower flute‑count tools.
- CNC milling on machining centers and vertical mills in job shops, mold shops, and general metalworking environments, including typicaldie & mold applications and general machining.
This 4 flute end mill is less suitable for very deep full‑slot cutting in soft, gummy materials, where chip evacuation is more critical and 2‑ or 3‑flute tools generally perform better
Buying Considerations
- Match the tool to your operation: Choose this 4 flute end mill when your main operations are side milling, step milling, and square shoulder machining rather than heavy full‑slot roughing.
- Check diameter tolerance vs. drawing:
- For features below 12 mm diameter, confirm that 0 / −0.02 mm tolerance meets your fit requirements.
- For 12 mm and above, ensure 0 / −0.03 mm tolerance is acceptable for your shoulders and slots.
- Confirm machine and fixturing rigidity: A 4 flute end mill performs best on rigid setups; if your machine or fixturing is flexible, you may need lighter radial engagement and reduced cutting data.
- Verify material and coating: Make sure the carbide grade and coating (if applied) are suitable for your workpiece material and cutting conditions. For hardened steel applications, you can also refer to the dedicated hardened steel end mill series as a comparison point.
- Select appropriate length: Avoid tools that are much longer than needed; excessive overhang increases deflection and chatter, reducing tool life and part quality
Selection Guide
- Define workpiece material and hardness
- For carbon steels, alloy steels, and cast irons in general machining, a standard 4 flute end mill geometry is suitable.
- For tougher stainless steels or higher hardness, consider coated versions or geometries optimized for those materials.
- Choose diameter and tolerance
- Select the cutter diameter according to slot width, step width, or required shoulder location.
- Use 0 / −0.02 mm for high‑precision features below 12 mm, and 0 / −0.03 mm for larger shoulders and steps where slightly more clearance is acceptable.
- Set length and overhang
- Choose a cutting length that covers your maximum axial depth of cut, and keep tool overhang as short as possible.
- For higher walls, use multiple step‑downs instead of one very deep pass to maintain stability.
- Plan the cutting strategy
- Use the 4 flute end mill primarily for side milling and finishing; use roughing tools with fewer flutes for heavy stock removal.
- Combine low to moderate radial engagement with adequate feed per tooth to maintain proper chip thickness and avoid rubbing.
If you need help building a complete tool set for your CNC machines, you can refer to the carbide end mill set selection guide for additional selection tips across different series.
Failure Case
A machine shop attempted to rough a full‑width slot in mild steel using a 4 flute end mill at a large axial depth and aggressive feed. Because the flute valleys on a 4 flute tool are smaller than on 2‑flute cutters, chips quickly packed in the slot and could not evacuate efficiently. Cutting forces increased sharply, the tool began to chatter, visible marks appeared on the slot walls, and the end mill suffered rapid flank wear and edge chipping before the feature was complete.
After reviewing the failure, they changed the process. Roughing was done with a 2‑ or 3‑flute roughing end mill at reduced axial depth per pass, which improved chip evacuation. The 4 flute end mill was then used only for side milling and finishing at lower radial engagement. This change eliminated chip packing, improved surface finish, and extended tool life significantly. If you frequently switch between roughing and finishing on steel parts, consider pairing this tool with a dedicated roughing end mill in your process planning.
What is a 4 flute end mill mainly used for?
A 4 flute end mill is mainly used for side milling, step milling, and square shoulder machining on steels and general engineering materials where good surface finish and dimensional accuracy are required
Can I use a 4 flute end mill for deep full‑slot cutting?
It is not ideal for very deep full‑slot cutting in materials that produce heavy chips, because smaller flute valleys can cause chip packing; 2‑ or 3‑flute tools are usually better for that kind of roughing.
Should I use a 4 flute end mill for roughing or finishing?
A 4 flute end mill can handle light to medium roughing but is best suited to semi‑finishing and finishing, while heavy stock removal and deep slots are usually better done with lower flute‑count roughing tools.
A VISIBLE QUALITY. YOU CAN BE TRUSTED.
01
Please confirm the tool size, coating type, and material compatibility before placing an order.
02
Carbide end mills are fragile – avoid impact and store them in a dry, secure place.
03
Ensure proper cutting parameters (speed, feed, depth) for best performance and tool life.
04
Wear safety protection (goggles, gloves) when operating cutting tools.
05
If you’re not sure which type to choose, feel free to contact us for professional recommendations.
Purchase Information
After-sales Support: We offer technical guidance and quick response for any product or usage concerns.
MOQ & Customization: Most models are in stock. Custom logo, size, or packaging is available – please consult before ordering.
Shipping: We support express, air, and sea shipping. Delivery time may vary by region and quantity.
Quality Assurance: All tools are inspected before shipment. We provide SGS and ISO certificates upon request.
Returns & Warranty: Defective or damaged products due to manufacturing issues can be replaced.
Customer Review Average rating: 4.7/5 based on our internal product evaluation for material grade consistency, cutting edge finish, and dimensional accuracy. This 4mm 4 flute solid carbide end mill is designed for stable side milling and slotting. It offers reliable cutting performance, good wear resistance, and consistent geometry for industrial machining applications. Reviewed by JYC Carbide technical team. Last updated: 2026-05-25.4mm 4 Flute Solid Carbide End Mill

4 flute solid carbide end mill for side milling and slotting, available in 4, 6, 8, 10, 12, 14, 16, 18, 20 mm diameters.
Product SKU: NCG-4E-DE01-20
Product Brand: JYC Carbide
Product Currency: USD
Product Price: 5
Price Valid Until: 2036-05-25
Product In-Stock: InStock
4.67




Request a Quote for Carbide Tools