2-Flute Ball End Mill for Precision 3D Contouring
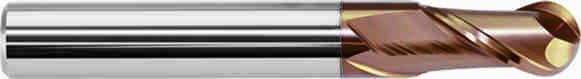
A 2-flute ball end mill designed for precision 3D contouring and complex surface finishing in hardened materials. The NCP-2B series features 30° spiral angle geometry, AlTiN coating, and is suitable for machining hardened steels (HRC45-55 depending on cutting conditions), mold materials (NAK80, P20), and aerospace alloys. The two-flute design provides efficient chip evacuation and reduced cutting forces compared to 4-flute variants, making it ideal for die & mold machining where surface finish Ra 0.4-0.8μm is typically achievable under controlled conditions.
Product Overview


The NCP-2B series ball nose end mill covers nose radius from R0.5mm to R10.0mm across 24 standard configurations. All tools feature integral cemented carbide construction (YK25SF substrate), 2-flute geometry, and TiAlXN coating for extended tool life in hardened materials. This design prioritizes chip evacuation and surface quality over metal removal rate, making it suitable for semi-finishing and finishing operations in aerospace component finishing and precision mold cavities.
Production capacity: 50,000 pieces/month | Customization: OEM coating, non-standard ball radius, extended length available upon request.
Technical Specifications
| Parameter | Specification |
| Product Series | NCP-2B |
| Product Type | Ball Nose End Mill |
| Application | 3D Contouring, Finishing, Profile Milling |
| Flute Count | 2 Flute |
| Coating | TiAlXN (AlTiN variant available) |
| Material | Micro-grain Cemented Carbide |
| Substrate Grade | YK25SF |
| Structure | Integral Solid Carbide |
| Ball Radius (R) | 0.5 – 10.0mm |
| Cutting Diameter (D) | 1.0 – 20.0mm |
| Spiral Angle | 30° |
| Overall Length | 50 – 100mm |
| Tolerance | ±0.005 to 0.01mm |
| Hardness Capability | Up to HRC55 (material and condition dependent) |
| Runout | <0.003mm |
| Suitable Process | Semi-finishing, Finishing |
| CNC Compatibility | All CNC Machining Centers |
| Customization | OEM, ODM, Custom Coating |
| MOQ | Flexible (Contact for details) |
| Production Capacity | 50,000 pieces/month |
| Packaging | Plastic Box / Custom Packaging |
| Brand | Jin Ta Pai |
| Origin | China |
| HS Code | 8207709000 |
When to Use 2-Flute Ball End Mills
Choose 2-flute ball nose cutters over 4-flute variants when:
- Deep cavity machining with limited chip space (L/D ratio >3:1)
- Finishing operations where surface quality prioritizes over removal rate
- Softer materials (aluminum, copper, graphite) where chip welding risk is high
- Older or less rigid machines where chatter suppression is critical
For harder materials (HRC52-62) with optimized geometry, consider the Hard Material Specific Two Blade Ball End Mill. For deep pockets requiring extended reach (L/D >5:1), see the Long Shank Ball End Mill variant.
Technical consultation: Share your material grade + hardness + tool diameter + spindle RPM limit + coolant type/pressure + tool overhang (L/D ratio). We provide conservative/optimal/aggressive parameter sets within 24 working hours.
Dimensional Standards: NCP-2B Series
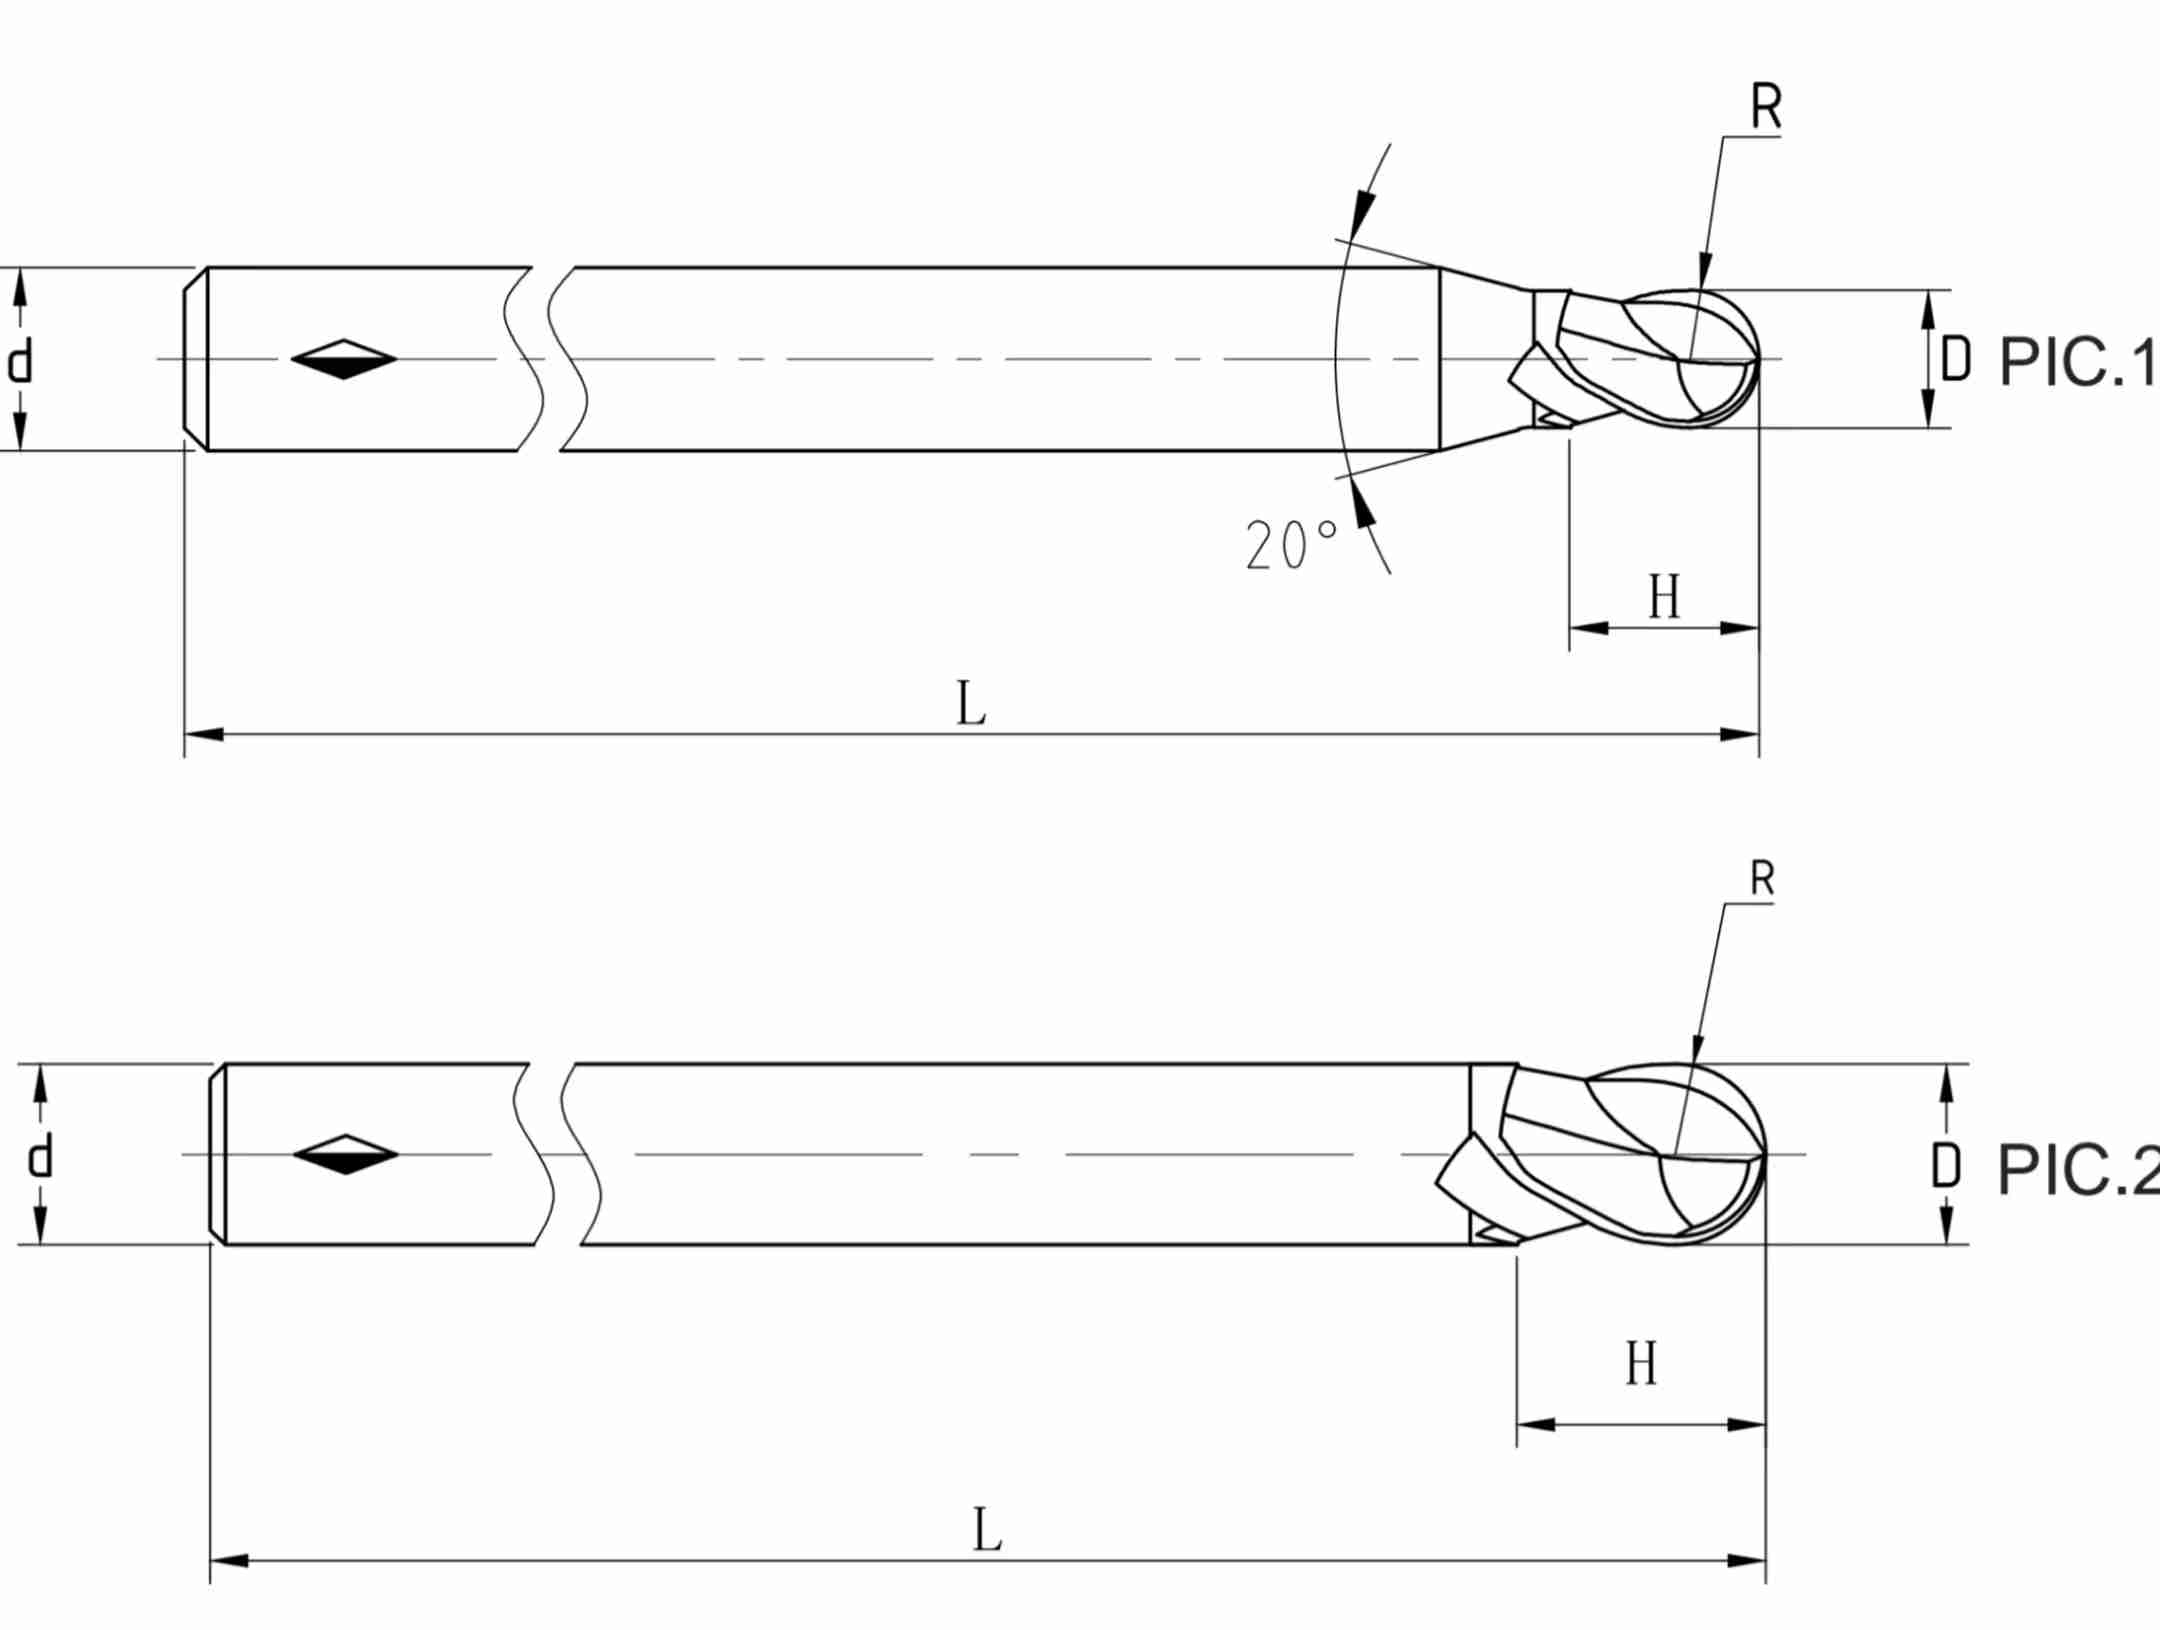
The table below lists 24 standard configurations covering micro-diameter (R0.5mm) to standard sizes (R10.0mm). Custom ball radii, extended lengths, and non-standard shank diameters are available with MOQ negotiation.

| Ball Radius (R) | Cutting Diameter (D) | Shank Diameter (d) | Flute Length (H) | Overall Length (L) | Recommended Material |
|---|---|---|---|---|---|
| R0.5 | Ø1 | Ø4 | 2 | 50 | Aluminum, Copper, Graphite |
| R1.0 | Ø2 | Ø4 | 4 | 50 | Mold Steel (HRC45-50), Aluminum |
| R1.5 | Ø3 | Ø4 | 6 | 50 | NAK80, P20, Aluminum |
| R2.0 | Ø4 | Ø4 | 8 | 50 | Hardened Steel (HRC50-55), Stainless |
| R2.5 | Ø5 | Ø6 | 10 | 50 | Tool Steel, Stainless Steel |
| R3.0 | Ø6 | Ø6 | 12 | 50 | Hardened Steel, Cast Iron |
| R4.0 | Ø8 | Ø8 | 16 | 60 | General Purpose, Mixed Materials |
| R5.0 | Ø10 | Ø10 | 20 | 75 | Large Cavities, Lower Hardness |
| R6.0 | Ø12 | Ø12 | 24 | 75 | Die Cavities (HRC45-50) |
| R8.0 | Ø16 | Ø16 | 32 | 100 | Automotive Dies, Large Molds |
| R10.0 | Ø20 | Ø20 | 40 | 100 | Heavy Roughing to Semi-finish |
Note: Lead time for standard sizes: 3-5 working days. Custom configurations: 7-15 working days depending on complexity.
Recommended Cutting Parameters
Starting parameters for NCP-2B series in common materials. Adjust based on machine rigidity, coolant pressure (minimum 15 bar recommended), and actual tool overhang.
| Material | Hardness | Cutting Speed (Vc m/min) | Feed per Tooth (fz mm) | Axial Depth (ap mm) | Radial Engagement (ae %) |
|---|---|---|---|---|---|
| Aluminum Alloys | 6061-T6 | 150-250 | 0.03-0.06 | 0.2-0.5 | 5-20% |
| Mold Steel | HRC28-35 | 80-120 | 0.02-0.04 | 0.1-0.3 | 5-15% |
| Hardened Steel | HRC45-50 | 60-90 | 0.015-0.025 | 0.05-0.15 | 3-10% |
| Hardened Steel | HRC50-55 | 40-70 | 0.01-0.02 | 0.05-0.1 | 2-8% |
| Stainless Steel | 304/316 | 50-80 | 0.02-0.035 | 0.1-0.2 | 5-12% |
| Titanium Alloy | Ti-6Al-4V | 30-50 | 0.015-0.03 | 0.05-0.15 | 3-8% |
Conditions: High-pressure coolant (15-30 bar), CAM toolpath with trochoidal engagement, runout <0.005mm. Surface finish results vary with machine stability and actual cutting conditions.
Troubleshooting Guide
| Failure Mode | Possible Causes | Corrective Actions |
|---|---|---|
| Premature nose wear | Excessive cutting speed; inadequate coolant pressure | Reduce Vc by 20%; increase coolant to 20+ bar; verify coating integrity |
| Chatter marks on surface | Tool overhang too long; low spindle RPM | Reduce L/D ratio <3:1; increase RPM by 15-25%; use damped tool holder |
| Nose chipping | Interrupted cuts; machine vibration | Add lead-in/lead-out moves; check spindle bearings; reduce ae to <5% |
| Poor surface finish (Ra >1.0μm) | High feed rate; runout >0.005mm; worn tool | Reduce fz by 30%; re-measure runout; replace tool if flank wear >0.15mm |
| Rapid flank wear | Hardness exceeds HRC55; dry cutting | Verify material hardness; switch to flood coolant; consider coated grade upgrade |
For complex failure analysis, refer to Ball Nose End Mill Mastery for case studies on HRC55+ machining.
Frequently Asked Questions
When should I choose 2-flute over 4-flute ball end mills?
Select 2-flute designs for finishing operations where chip evacuation is critical (deep cavities, soft materials like aluminum or copper, or machines with limited coolant pressure). Choose 4-flute for semi-roughing in stable setups with high coolant flow and rigid machines.
What is the maximum L/D ratio for the NCP-2B series?
Standard configurations support L/D ratios up to 4:1. For deeper reach (L/D 5:1 to 8:1), specify extended-length variants or consider our long-shank series with reinforced core diameter.
How do I avoid chipping the ball nose during entry/exit moves?
Use helical or ramping entry strategies with lead angles 2-5°. Ensure CAM software generates tangent lead-in/out moves (minimum arc length 2× ball radius). Avoid plunge cuts perpendicular to the surface.
Can I request custom ball radii not listed in the standard table?
Yes. Custom ball radii (e.g., R0.75mm, R3.5mm) are available with MOQ typically 20-50 pieces depending on diameter. Lead time: 10-15 working days. Provide target radius ±0.005mm tolerance requirement.
What is the difference between TiAlXN and AlTiN coatings?
TiAlXN (standard NCP-2B coating) offers balanced wear resistance and oxidation stability up to 800°C, suitable for general hardened steel machining. AlTiN variant provides higher hardness (HV 3200+) and better performance in continuous high-speed cuts but may be more brittle in interrupted operations. Specify coating preference at order.
Request Custom Quote
For Engineers: Share material grade + hardness (HRC) + required ball radius + spindle speed limit (RPM) + coolant type/pressure (bar) + tool overhang (L/D ratio). We provide within 24 working hours: recommended tool spec, conservative/optimal/aggressive cutting parameters, and failure troubleshooting checklist. Contact technical support.
For Procurement: Provide specification (ball radius + quantity + delivery timeline). We respond within 24 hours with pricing, support OEM branding, custom packaging options, and provide material certificates and inspection reports upon request. Submit RFQ.


Request a Quote for Carbide Tools